4 Jaw Self - Centering Chuck
 Owner’s Manual
for the VM90, VM100,
VM120, VM140 &
VM150
Vicmarc Machinery Pty Ltd Manufacturers of Quality Woodturning Lathes and Accessories
Vicmarc Machinery Pty Ltd
52 Grice Street Clontarf QLD 4019 Australia
Phone (07) 3284 3103 Int Ph 61-7 3284 3103 Email vicmarc@vicmarc.com
Fax (07)3283 4656 Int Fax 61-7 3283 4656 Web www.vicmarc.com
Manufacturers of Quality Woodturning Lathes, Chucks and Accessories
Vicmarc Machinery, a family owned and operated business, has been manufacturing wood turning lathes and accessories for the hobbyist and professional since 1984. The company is dedicated to providing machinery of the highest quality and precision engineering which has secured sales worldwide.
Through constant improvement, Vicmarc retains its place as a leader in the field. Vicmarc lathes and chucks are known and respected internationally for their robust design and ease of use. Only the best materials and latest high precision, computer controlled machinery are used in the manufacture of Vicmarc products.
The company continues to respond to the demands of the market, updating and improving at all stages of manufacture.
Description
The Vicmarc 4 Jaw Self Centering Chuck is designed and manufactured in Australia by Vicmarc Machinery, utilising the precision, simplicity and reliability of the engineering chuck.
This chuck grips internally and externally, will hold round and square work, has a hollow centre so that through boring can be done from either end and can even be run clockwise or anticlockwise.
Manufactured from K1045 (medium tensile steel - 45 tonne) the chucks have a higher durability ensuring a longer life and a very high quality finish which is less susceptible to rust.
Vicmarc chucks are guaranteed for 12 months and a large variety of accessories are available to suit them.
I MPORTANT SAFETY INFORMATION
Vicmarc wood turning chucks are manufactured from the highest quality materials to ensure a long working life. To ensure that your chuck is kept at its optimum performance please take note of the following points:
-
All Vicmarc chucks have a stop pin below the number No. 4 jaw runner except the VM150 which has the stop pin below the No. 2 Jaw. Its purpose is to prevent the jaws from expanding beyond the safe working limit. The chuck must NOT be opened beyond its full extent or damage could be caused to the stop pin. A damaged Stop Pin could in turn damage the Jaw Runners. We recommend the use of a larger dovetail jaw set when working with larger scaled pieces.
-
The "Screw Point" supplied with each Vicmarc Chuck should be mounted as described in the Owners Manual (page 6). Failure to mount the screw correctly could cause damage to the screw point. Drilled holes for the screw point should be as follows: 7mm - 7.5mm for Softwoods 8mm - 8.5mm for Hardwoods Where possible, holes should be drilled on a pillar drill.
List of Contents
- Safety Precautions ........ Page 4
- Maintenance ........ Page 5
- Beginners Tips ........ Page 5
- Mounting on the Lathe, Clamp Mode, Expansion Mode ........ Page 6
- Operation - VM90 & VM140 ........ Page 7
- Operation - VM100 & VM120 ........ Page 8
- Operation - VM150 ........ Page 9
- Maintenance - VM150 ........ Pages 11-13
- Jaw Styles and Accessories ........ Pages 14-17
- Exploded Diagram Chuck Jaws ........ Pages 18-19
- The Vicmarc Guarantee ........ Page 20
SAFETY PRECAUTIONS
-
READ AND UNDERSTAND INSTRUCTION MANUAL BEFORE OPERATING WOOD LATHE.
-
Always wear eye protection.
-
Do not wear gloves, neckties, jewellery or loose clothing.
-
Do not operate without guards in place.
-
Rough out workpiece before installing on face plate.
-
Do not mount a split workpiece or one containing a knot.
-
Tighten all locks before operating.
-
Rotate workpiece by hand before applying power.
-
Use slowest speed when starting a new workpiece and do not exceed permitted speed.
-
Disconnect machine from power source before making repairs or adjustments.
-
Do not operate while under the influence of drugs alcohol or medication.
-
Remove the tool rest before sanding or polishing.

GENERAL MAINTENANCE
Before the chuck is mounted on the lathe, make sure that all the threads are thoroughly clean and free of debris. This will ensure the chuck will run true.
The chuck is engineered to very close tolerances and may initially be stiff to operate. With use movement will become easier. To maintain easy jaw action, regularly spray oil onto the scroll and work lever through full range of movement. Inspect chuck regularly for build up of dust in the scroll and jaws. Clean as required.
BEGINNERS TIPS
PREPARE THE WORK PIECE THE FOLLOWING WAY
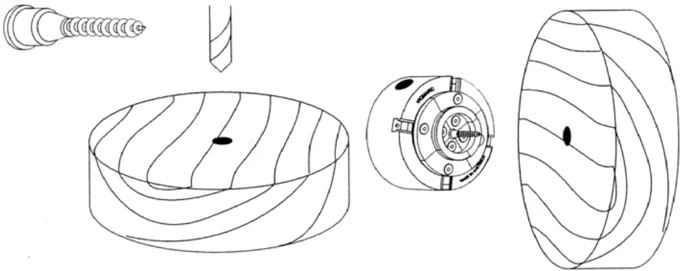
200-250mm dia. 40-50mm thick; RPM 800-1000
- Drill 25mm deep and 7-8mm dia. hole in the centre of workpiece (Avoid drilling into the end grain, this could result in less grip)
- Make sure the workpiece is as round as possible.
- Choose appropriate speed before you start the lathe.
- Screw the workpiece hard against the jaws.
- Heavy or unbalanced workpieces should not be fastened directly to the screw chuck. Use the face plate rings instead.
Mounting on the Lathe
The Vicmarc Uni-Chuck fits a wide range of lathe spindle sizes. This is done by changing the threaded insert. Your dealer will advise on the insert required for your lathe. Check that the insert is firmly screwed into the Chuck body and then screw the assembled chuck into the lathe spindle. Insert must be firmly seated against the lathe spindle shoulder.
 Insert
Lathe Spindle
Chuck
The Screw Point
The Screw Chuck is used to mount small cross grained pieces
 Backing Jaws
Standard Jaws
Screwpoint
Clamp Screw Point this way for VM90 & VM 100
Clamp Screw Point this way for VM120, VM140 & VM150
Clamp Mode
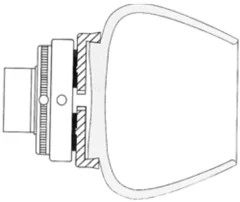
With this application the workpiece is held by the jaws. To achieve a good hold, press the bowl end hard against the jaws. Fasten the workpiece to the screw or onto the face plate. When pre-turning bowls from green timber it is possible to do this between centres or with a pivot chuck. Turn a 5 to 10mm deep dovetail recess first. The sizes of all the jaw types available are shown in the tables on pages 18 and 19.
Expansion Mode
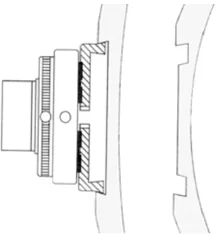
For this application a recess is turned into the workpiece. The depth of the recess depends on the actual size of the workpiece as well as the type of timber used. The minimum depth should be 5mm to 10mm
OPERATION
V M90 and VM140
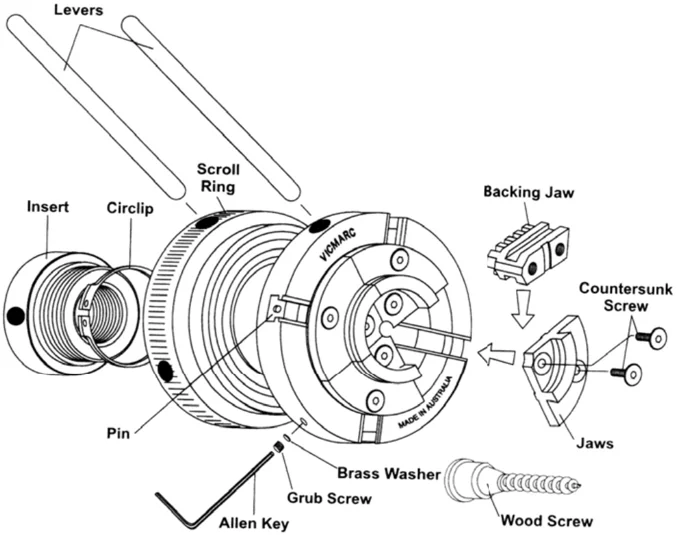
The VM90 and VM140 chucks are for those who prefer to operate the chuck using the quick- acting Tommy Bars (Levers), which saves time when mounting and dismounting bowls.
The VM90’s compact size makes it ideal for use on 300mm (12”) capacity lathes or smaller, whilst the VM140 will hold most work up to 500mm (20”) in diameter with standard jaws.
The basic chuck includes: chuck body, two tommy bars, screw point, allen key, and the owners manual.
OPERATION
VMI100 and VMI120
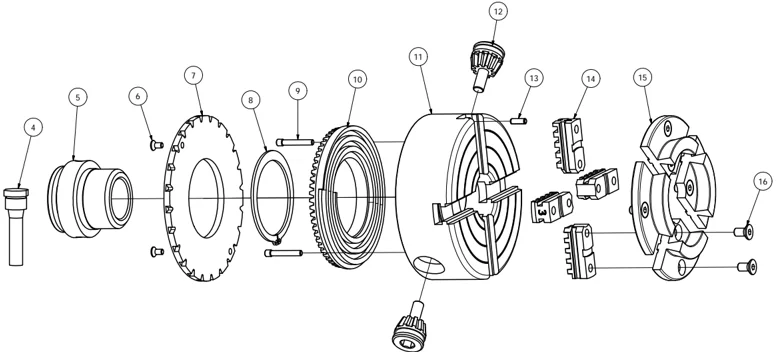
The VMI100 and VMI120 t-bar allen key operated chucks provide one-hand tightening along with tremendous gripping power provided by the 6 to 1 ratio of the scroll. The totally enclosed back assures a consistent smooth action by preventing dust and debris from getting into the scroll of the chuck.
Keyed chucks cannot be beaten when it come to holding power.
The VMI100’s compact size makes it ideal for use on 300mm (12”) capacity lathes or smaller, whilst the VMI120 will hold most work up to 500mm (20”) in diameter with standard jaws.
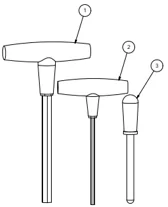
Basic chuck includes: chuck body, t-bar allen key, screw point allen key and the owners manual.
PARTS LIST
| ITEM | QTY | VM100 - PART NUMBER | VM100 - DESCRIPTION | VM120 - PART NUMBER | VM120 - DESCRIPTION |
|---|---|---|---|---|---|
| 1 | 1 | P00027 | 8mm T-Bar | P00028 | 10mm T-Bar |
| 2 | 1 | P00024 | 3mm T-Bar | P00025 | 4mm T-Bar |
| 3 | 1 | V00093 | 7.9mm Tommy Bar | V00091 | 9.5mm Tommy Bar |
| 4 | 1 | V00991 | Wood Screw | V00991 | Wood Screw |
| 5 | 1 | - | Insert VM90-100 | - | Insert VM120-150 |
| 6 | 2 | P00719 | M4 x 8 Screw, Socket Flat Head | P00719 | M4 x 8 Screw, Socket Flat Head |
| 7 | 1 | V00178 | VM100 Backing Plate | V00178 | VM120 Backing Plate |
| 8 | 1 | P00249 | 50mm External Circlip | P00251 | 60mm External Circlip |
| 9 | 2 | P00591 | M5 Dowel Pin | P00591 | M5 Dowel Pin |
| 10 | 1 | V01000 | VM100 Scroll | V01001 | VM120 Scroll |
| 11 | 1 | P00972 | Chuck Body, M40x2 | P00997 | Chuck Body, M45x2 |
| 12 | 2 | V00900 | VM100 Pinion | V00901 | VM120 Pinion |
| 13 | 1 | P00598 | Roll Pin Dia 3 x 10mm | P00599 | Roll Pin Dia 4 x 12mm |
| 14 | 1 | V00637 | VM100 Backing Jaws | V00670 | VM120 Backing Jaws |
| 15 | 4 | V00657 | VM90-100 Standard Jaws | V00695 | VM120-150 Standard Jaws |
| 16 | 8 | P00720 | M5 x 12 Screw, Socket Flat Head | P00725 | M6 x 12 Screw, Socket Flat Head |
OPERATION
VMI50
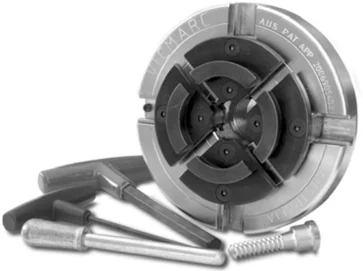
The VMI50 Chuck is a new and innovative patented design with many exceptional features for the professional turner or the serious hobbyist. Jaws and inserts are compatible with the VMI20 but the backing jaws have been made larger and stronger to withstand very heavy use.
The VMI50 is ideal for use on 400mm (16") capacity lathes or larger.
The basic chuck includes: chuck body, one tommy bar, screw point, 2 x allen keys, and the owners manual.
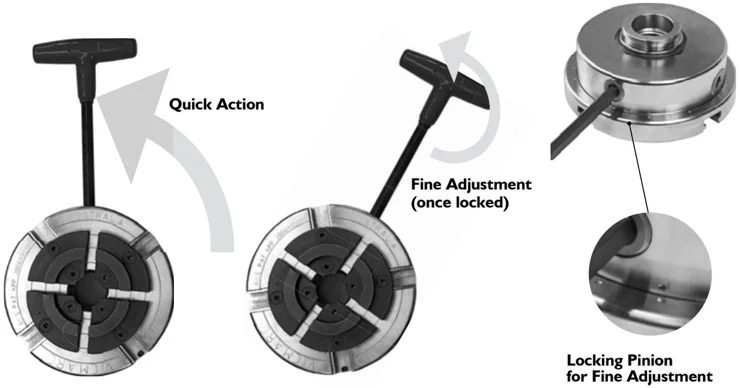
VMI50 Features
Quick Action
Fine Adjustment (once locked)
Locking Pinion for Fine Adjustment
The VMI50 is a revolution in chuck design from Vicmarc. To save you time and energy this chuck has two actions - one to rapidly open and close the chuck as though it was lever operated (fully open in 3 revolutions), the other to tighten using the 'T' Key as you would in a standard key operated scroll chuck. To switch from lever operated to key operated, line up the dots as shown above and rotate the locking pinion using the 10mm T-bar (supplied) Turn clockwise to engage and anti-clockwise to disengage.
OPERATION
Compatible with VM120/140 Jaws
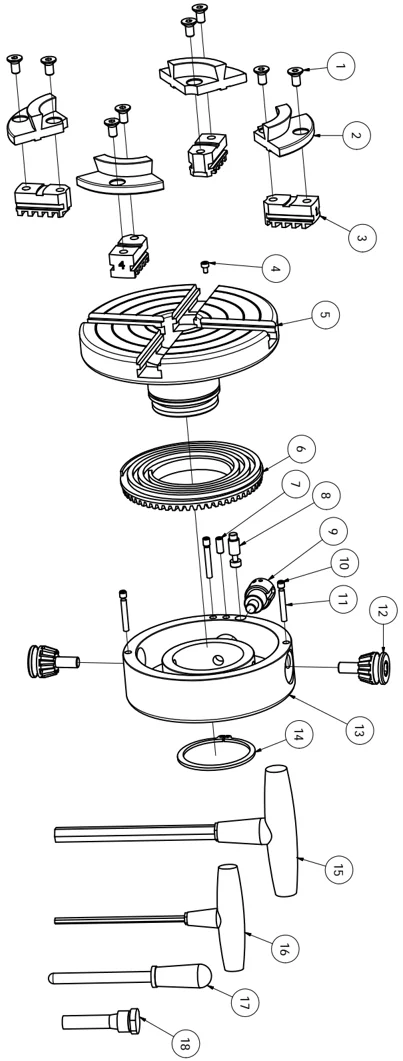
PARTS LIST
| ITEM | QTY | PART NUMBER | DESCRIPTION |
|---|---|---|---|
| 1 | 8 | V00997 | M6 x 12 Screw, Socket Flat Head |
| 2 | 4 | V00695 | Jawset, VM120/140 Standard |
| 3 | 1 | V00697 | Backing Jawset |
| 4 | 1 | P00737 | M3 x 5 Socket Head Cap Screw |
| 5 | 1 | Chuck Body, VM150 | |
| 6 | 1 | V01001 | Scroll |
| 7 | 1 | M5 x 12 Ball Catch | |
| 8 | 1 | V00886 | Locking Pin |
| 9 | 1 | Locking Pinion |
PARTS LIST
| ITEM | QTY | PART NUMBER | DESCRIPTION |
|---|---|---|---|
| 10 | 3 | P00738 | M5 x 5 socket set screw |
| 11 | 3 | P00590 | Pin, Dowel 4x25 |
| 12 | 2 | V00901 | Pinion |
| 13 | 1 | P00250 | Chuck Housing, VM150 |
| 14 | 1 | P00028 | 55mm external circlip |
| 15 | 1 | P00025 | 10mm T-Bar |
| 16 | 1 | V00091 | 4mm T-Bar |
| 17 | 1 | 9.5mm Tommy Bar | |
| 18 | 1 | V00991 | Chuck Wood Screw |
MAINTENANCE
VMI50 Chuck Accessories
Before undertaking any maintenance work to the VMI50 chuck please familiarise yourself with the individual parts and the correct terminologies.
VMI50 Backing Jaw Indentification
Each jaw should be individually numbered. Should the numbers become obscured the jaws can be easily indentified by the scroll patterns shown below.
Top
Bottom
Jaw 1 Jaw2 Jaw 3 Jaw 4
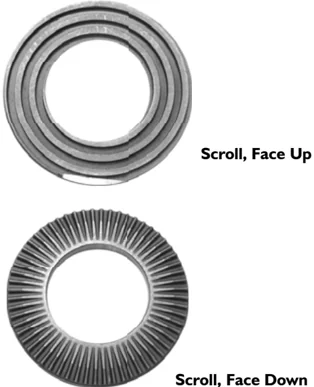
VMI50 Scroll
 Scroll, Face Up
Scroll, Face Down
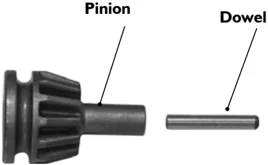
VMI50 Pinions
Pinion Dowel
MAINTENANCE
VM150 Back Jaw Mounting Sequence
 Stop Screw
Jaw 4
Jaw 1
Jaw 3
Jaw 2
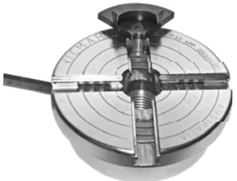
All the backing jaws are numbered to ensure easy assembly. The number two jaw is where the stop screw is as pictured on the left.
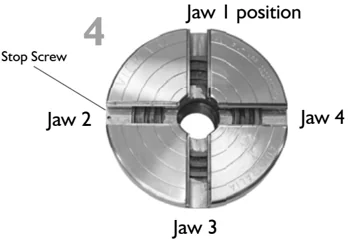
Before commencing it is better to orientate the chuck so that the stop screw is on your left. Then begin to feed the jaws on from No.1 at the top and continue in an anticlockwise direction as shown below.
VM150 Dismantling
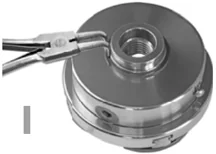
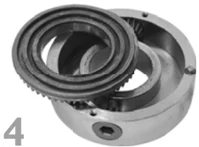
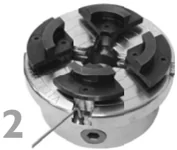
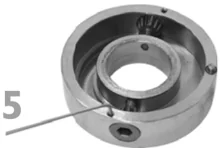
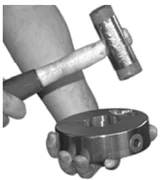
To begin dismantling the VM150 chuck, place it on a clean bench with the back facing up. 1 Remove the circlip. 2 Turn the chuck over so that the jaws are now upright. Undo and remove the stop screw situated by jaw two. 3 Slide all the jaws out. 4 Pull off the frontplate to show the inside of the chuck. The scroll can then be removed from the backplate. 5 To remove the pinions from the backplate first remove the grub screw that holds the dowel in, then turn the back plate so that the dowel that holds the pinion is facing downwards. 6 Gently tap the back plate with a soft hammer until the dowel drops out. You may then remove the pinion.
MAINTENANCE
VMI 50 Reassembling
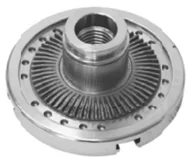
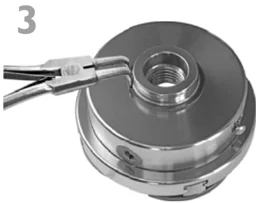
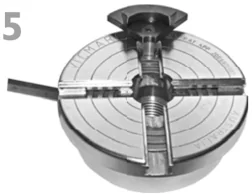
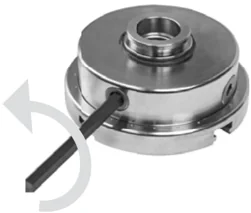
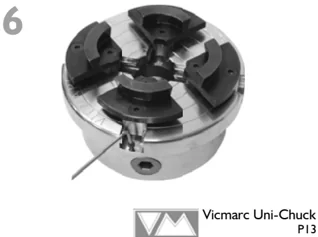
Make sure that all the components have been thoroughly cleaned and re greased before re assembly. 1. Place the front plate face down on a clean workbench. Then making sure the scroll face is pointing downwards with the gear (or gear teeth) facing upwards, drop the scroll into the body. 2. Put the backing plate on - do not force this together as the gear may be damaged. Place the allen key into the pinion and slightly rotate until the teeth mesh and the circlip groove becomes visible. 3. Replace circlip. 4. Turn over the chuck. Then rotate the scroll until the start of the scroll thread is in the number one position as shown in picture. 5. Replace jaw number 1, rotate 1/4 revolution anticlockwise, replace jaw number 2, rotate 1/4 revolution and so on until all the jaws are replaced. 6. Once the scrolls have been replaced, rotate the allen key until the screw hole at jaw number two becomes visible. Screw in the stop screw ensuring that it is not over tightened.
JAW STYLES and ACCESSORIES
This is a sample of the Vicmarc chuck jaws and accessories. For the full range see pages 18 to 19 to find the jaws that suit your requirements. These jaw styles suit all chucks types.
Step Jaws
Step Jaws, designed by the famous Australian woodturner and author Richard Raffan, are used for holding a range of spigot sizes with minimum jaw movement and without the necessity to change the jaws. Boxes are easily turned using the step jaws. The bottom can be turned by holding the rim without leaving unsightly pressure marks.

25mm Jaws
These jaws are used for expansion into small recesses and for firm holding of fine spindle work, such as earrings, chess pieces etc. They are ideal for turning salt and pepper shakers. To turn very small articles, the jaws can be unscrewed and the backing jaws only can be used.
Bowl Jaws
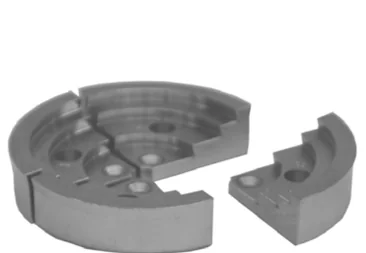
The adjustable jaws allow you to re-chuck bowls for finishing the bottom or do light clean-up work on the foot of the bowl. To mount the bowl, the bowl is reversed and held by the rim, either internal or external, with 8 unique soft plastic stoppers which are mounted on the face of the jaws. The numerous mounting holes on the face of the jaws allow you to locate the stoppers in any number of positions. The range of sizes listed on pages 18 and 19.
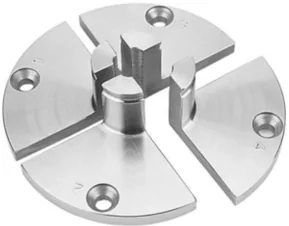
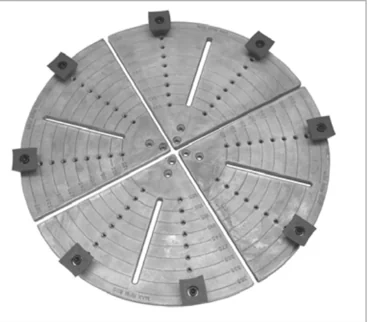
JAW STYLES and ACCESSORIES
Long Nose Jaws
These jaws allow better access between the chuck body and the rear of the workpiece. They are also very practical when pre-turned workpieces or long workpieces have to be refastened. For example, when turning serviette rings or remounting rough turned work.
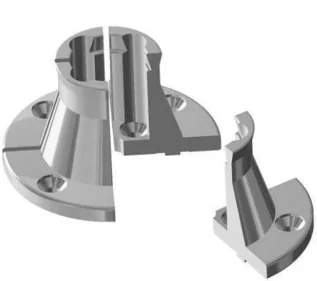
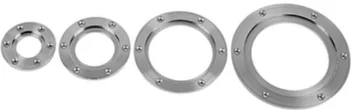
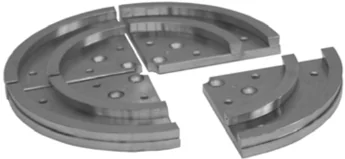
Face Plate Rings
These can be used instead of the traditional faceplate. They facilitate remounting of prepared blanks by mounting directly onto the chuck jaws. Also can be used for turning green wood which will require returning later on. Fit standard jaws supplied on chuck.
Shark Jaws
Shark jaws are so called because of their serrated inner and outer jaw surfaces. These extended jaws provide an aggressive hold. They hold cylinder spigots much more safely than standard jaws. They are easier and faster than traditional jaws used to turn long workpieces.
Available in 48mm to 88mm for the VM90 and VM100, 55mm to 130mm for the VM120, VM140 and VM150.
JAW STYLES and ACCESSORIES
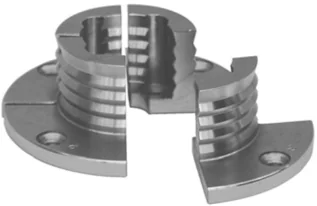
Dovetail Jaws
Dovetail jaws are designed for mounting bowls by expanding into a recess or by clamping onto a spigot. The size indicated is the outside measurement of the jaw face when fully closed. Dovetail jaws provide approximately 25mm of expansion beyond their specified size.

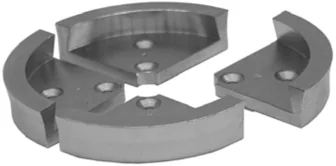
Multi - Purpose Jaws
By removing one or more of the dovetail segments from these jaws, they are adaptable to a variety of uses. The wide range of expansion and contraction of the Uni-Chuck provides for unique adaptability when using these jaws.
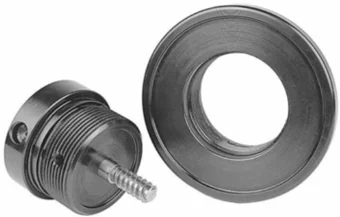
3 - in - I Screw Face Plate
This screw chuck has three alternative diameters of 50mm, 75mm and 100mm to give optimum support to any size of work. Made from K1045 medium tensile steel. Fitted with the Glaser screw. Fits most lathes. Alternative thread sizes available by using Vicmarc® chuck inserts. Some direct threads also available.
JAW STYLES and ACCESSORIES
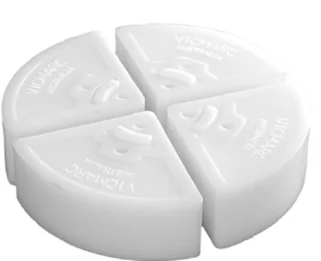
Soft Jaws
Would you like to turn your own custom made jaws to suit your work piece? Now you can do it with the all new Vicmarc Acetyl Soft Jaws. They are a convenient and simple to use accessory. As the jaws can be turned precisely to suit the job, the work piece will always be true and concentric. Jaws can also be drilled, sawn or tapped. Two sizes are available - 125mm and 150mm.
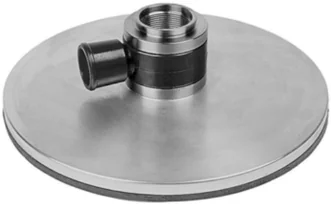
Vacuum Plate
This device has been designed as an aid to woodturning. It enables an item to be re-mounted on the lathe for finishing without risking further holding marks. This device can be fitted directly into a Vicmarc® chuck via the standard jaws, or an insert can be supplied as an extra to allow mounting directly onto the spindle. Size - 300mm.
All measurements listed refer to the outside diameter.
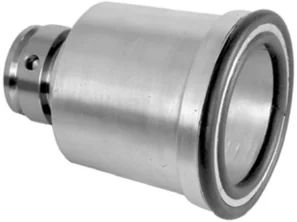
Vacuum Chuck
Precision machined cast aluminium. Each cylinder includes two soft 'o' ring seals for internal or external pickups. This unit works in conjunction with the Vacuum Plate, fitted with a rotary vacuum adaptor that connects to a shop or domestic vacuum. The rotary adaptor is fitted with two ball bearings and lets the lathe spindle turn freely while the hose and connection remain stationary.
| EXP MODE | 47 | 72 | 99 | 99 | 144 | 25 | 35 | 36 | - |
|---|---|---|---|---|---|---|---|---|---|
| VM90 VM100 | |||||||||
| STANDARD | DOVETAIL 2 STEP 70mm | DOVETAIL 100mm | STEP | DOVETAIL 144mm | PIN 25mm | PIN 35mm | LONG NOSE | PEN BLANK JAW | |
| CLAMP MODE | 33 | 55 44 | 83 | 84, 70 45 | 128 | EXPANSION ONLY | >7 | 25 | 10 sqr |
| PART NUMBER | V00657 | V00644 | V00642 | V00658 | V00643 | V00650 | V00651 | V00647 | V00659 |
VM90/100 JAW RANGE ALL MEASUREMENTS ARE DIA.(mm) OF JAWS ON PERFECT CIRCLE +38mm Jaw expansion, -2mm Jaw contraction
| 48 | 55 | 74 | 88 | 125 | 74 | 99 | 127 | 144-270 | 145-330 | 153-430 |
|---|---|---|---|---|---|---|---|---|---|---|
| SHARK 48mm | SHARK 55mm | SHARK 74mm | SHARK 88mm | PLASTIC 125mm | FACE PLATE RING 70mm | FACE PLATE RING 90mm | FACE PLATE RING 120mm | BOWL 220 | BOWL 285 | BOWL 385 |
| 35 | 42 | 60 | 74 | — | 46 | 70 | 100 | 95-220 | 95-270 | 105-375 |
| V00653 | V00654 | V00655 | V00656 | V00652 | V00400 | V00401 | V00402 | V00639 | V00640 | V00641 |
VICMARC MACHINERY P/L WWW.VICMARC.COM ISSUE-2015
VM120/140/150 JAW RANGE
ALL MEASUREMENTS ARE DIA.(mm) OF JAWS ON PERFECT CIRCLE
+48mm Jaw expansion, -2mm Jaw contraction
| EXP MODE | 68 | 105 | 128 | 148 | 173 | 198 | 223 | 127 | 25 | 35 | 47 |
|---|---|---|---|---|---|---|---|---|---|---|---|
| VM120 VM140 VM150 | |||||||||||
| STANDARD | DOVETAIL 105mm | DOVETAIL 128mm | DOVETAIL 148mm | DOVETAIL 173mm | DOVETAIL 198mm | DOVETAIL 223mm | STEP | PIN 25mm | PIN 35mm | LONG NOSE | |
| CLAMP MODE | 48 | 84 | 106 | 126 | 150 | 175 | 200 | 111, 97 70, 50 | >7 | >7 | 30 |
| PART NUMBER | V00695 | V00676 | V00677 | V00678 | V00679 | V00680 | V00682 | V00696 | V00687 | V00688 | V00684 |
| 55 | 68 | 83 | 130 | - | 150 | 74 | 99 | 127 | 168 | 145-360 | 153-460 | 158-555 |
|---|---|---|---|---|---|---|---|---|---|---|---|---|
| SHARK 55mm | SHARK 68mm | SHARK 83mm | SHARK 130mm | PEN BLANK JAW | PLASTIC 150mm | FACE PLATE RING 70mm | FACE PLATE RING 90mm | FACE PLATE RING 120mm | FACE PLATE RING 150mm | BOWL 285 max. 1000rpm | BOWL 385 max. 800rpm | BOWL 485 max. 600rpm |
| 35 | 48 | 65 | 110 | 15 sqr | — | 46 | 70 | 100 | 132 | 93-313 | 105-410 | 110-500 |
| V00692 | V00693 | V00694 | V00691 | V00698 | V00690 | V00400 | V00401 | V00402 | V00403 | V00672 | V00673 | V00674 |
VICMARC MACHINERY P/L
WWW.VICMARC.COM
 ISSUE-2015
Vicmarc Machinery Pty Ltd 52 Grice Street Clontarf QLD 4019 Australia
Phone (07) 3284 3103 Int Ph 61-7 3284 3103 Email vicmarc@vicmarc.com
Fax (07)3283 4656 Int Fax 61-7 3283 4656 Web www.vicmarc.comAAA
The Vicmarc® Guarantee
Vicmarc Machinery, manufacturers of Vicmarc machine tools, hereby guarantee the purchaser of the Uni - Chuck that the chuck was precision engineered from the finest materials available and was thoroughly inspected and tested before leaving the factory.
If, within 12 months following the date of delivery, the chuck is proven to have been defective as a result of faulty materials or workmanship, Vicmarc Machinery will repair or replace the chuck free of charge. This guarantee is subject to the following conditions:
- The chuck shall be returned to Vicmarc Machinery within 12 months with a brief description of the complaint.
- The name and address of the purchaser, together with the date of purchase and supplier details shall accompany the parts.
- Vicmarc Machinery will accept no responsibility whatsoever under the guarantee or otherwise if the chuck is not used strictly in accordance with the instructions supplied, or if the fault can reasonably be explained by carelessness or negligence.
- The purchaser is responsible for all costs incurred in transport and packaging to and from Vicmarc Machinery.
- In the case of accident, liability is expressly excluded when the chuck is tampered with or altered without authorisation.
Overseas purchasers are advised to obtain local guarantees from their Uni - Chuck agent. Conditions may vary to those detailed above.
Distributed by:
Aug 10 Edition